

『Flow Meter Prover System: Master Meter Benchmarks for On-Site Field Calibration』Related information(v cone flow meter|rotary gas meter|gallon meter|gear meter|metal tube rotameter|glass tube rotameter|nutating disk meter|transit time ultrasonic flow meter|wedge flow meter|pd meters|hydraulic flow meter|ultrasonic water flow meter|water flow meter|air flow meter|magnetic water flow meter|oxygen flow meter|gas flow meter|argon flow meter|air velocity meter|gasoline flow meter|fuel flow meter|ultrasonic water meter|digital water meter|nitrogen flow meter|solid flow meter|Oxygen tank flow meter|digital water flow meter|diesel fuel flow meter|steam flow meter|02 flow meter|compressed air flow meter|oil flow meter|liquid flow meter)
Flow Meter Prover System: Master Meter Benchmarks for On-Site Field Calibration
Quick Answer: A flow meter prover system with a master meter gives you on-site calibration without shutting down the line for days. It compares a field instrument against a high-accuracy reference meter, typically a Coriolis or electromagnetic type, in series on the same process fluid. Most teams can trace accuracy back to ISO 17025 within one shift and avoid the shipping cost and downtime of a fixed lab.
Why Plant Engineers Move to On-Site Master Meter Proving
Pulling a flow meter out of a live process line hurts. You drain product, bolt in a spare, rent a crane, and wait two weeks for a third-party lab report. A water utility in the Philippines told us they lost 3 days of billing data just to calibrate one DN200 electromagnetic meter. That is when we started configuring master meter packages that roll up on a trolley.
Here is the thing. Most custody transfer and batch control meters only drift a fraction of a percent. You do not always need a deadweight prover or a piston unit. A master meter reference with 0.1% or 0.15% uncertainty is enough for routine checks on vortex, oval gear, and turbine meters in oil, chemicals, and food lines. The field team verifies the device under test while the plant keeps running. That keeps both the maintenance manager and the production supervisor calm.
In remote locations across Australia, Southeast Asia, and East Africa, we see more sites adopting portable master meter provers. The reason is simple. Shipping a reference meter with a calibration certificate costs far less than moving the whole process meter to a capital-city lab every year.
How a Master Meter Prover System Works on Site
A master meter prover places the reference meter and the unit under test in series flow. The operator opens a bypass, isolates the section, and runs process liquid through both meters at the same time. You log pulses or 4-20 mA HART outputs from each instrument at 3 to 5 stable flow rates, usually covering 10%, 25%, 50%, 75%, and 100% of the operating range. Then you calculate the K-factor deviation for each point.
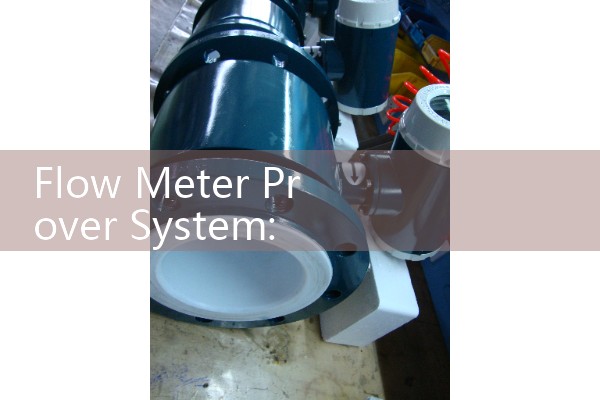
The reference master meter stays traceable to an accredited lab with a valid ISO 17025 certificate. Silver Automation Instruments typically supplies a Coriolis mass flow master for liquids from 0.5 cP to 500 cP. For conductive fluids, like demin water or caustic soda, we also configure a high-end electromagnetic master head. The reference meter sits in an easy-to-carry stainless steel tube section, complete with matched flanges RTD PT100 and a local totalizer so you do not need a separate flow computer on small jobs.
Most engineers skip this part on their first install, but orientation matters. A Coriolis master must stay full of liquid and free of two-phase flow. We recommend mounting the reference tube vertically with upward flow for brine and chemical applications, same as you would for a permanent installment. The master meter bench does the rest. Just connect the impulse lines or cables and start logging.
Key Specs We Size Every Day
We get RFQs that just say “need prover for 2 inch diesel line.” That is not enough. For a master meter skid you need to pin down five numbers before quoting a package:
Pipe size from DN10 up to DN250 and flow range in kg/h or m3/h. Process temperature in °C because the Coriolis sensor and PT100 have limits, especially on hot oil above 150 °C. Fluid name and viscosity in cP. A palm oil mill needs a different reference geometry than a solvent blending plant. Line pressure in bar, to spec the flange rating and tube wall thickness. Ex certification if the skid goes into ATEX Zone 1 or IECEx Zone 2. A paint manufacturer in Indonesia needed an EEx d purge system on their master meter trolley just to check a positive displacement meter inside a solvent room.
We have seen this on customer sites many times. If you skip the viscosity check, you will meter heavy fuel oil on a Coriolis master and scratch your head over a zero-shift at low flow. We simply ask you to send your pressure, temperature, pipe size, and flow range early. That lets our applications team pick the master type, line size, and connection standard so the whole trolley lands at your facility ready to bolt in.
Real-World Master Meter Benchmarks
Last year a customer in Vietnam asked us to help verify 18 oval gear flow meters on a marine fuel blending skid. They were operating at 80 °C wi
In a wastewater plant in Kenya, the operators were fighting an electromagnetic flow meter that read 6% high on sludge return. A quick inline master meter test using a battery-powered electromagnetic reference identified the grounding fault on site. They fixed the earth ring the same afternoon and avoided a premature meter replacement. That kind of diagnostic speed is what makes a master meter prover pay back fast.
For water abstraction and irrigation schemes in the Murray-Darling basin, we configure truck-mounted master provers that alternate between different line sizes from DN50 to DN300. The reference is a dual-beam ultrasonic clamp‑on master, accurate to 0.5% of reading, able to verify multiple meters in one day. Because the master is non-intrusive, the crew just clamps it and moves on. That is the approach that regulators in Australia now accept for annual compliance checks on bore meters.
Silver Instruments Master Meter Packages
Silver Automation Instruments builds master meter provers around the same sensors we sell for permanent installations. The reference line-up includes Coriolis mass flow meters, electromagnetic flow meters, and high-precision ultrasonic meters. Each master meter ships with a delta-T PT100 pair for density compensation when needed, a multi-variable transmitter with 4-20 mA HART and Modbus RTU output, and a rugged aluminium case for transport. We also supply a tablet-based logging app that computes average K-factor and repeatability right there at the test point, no laptop needed.
Because we supply directly to end users and distributors in Southeast Asia, Oceania, Latin America, Africa, and the Middle East, we size the skid for the local power supply, whether that is 24 V DC from a truck battery or 230 V AC mains. We avoid universal statements that do not fit the field. We build the trolley to match your environment: stainless steel frame for marine and offshore, carbon steel with epoxy coat for dry inland terminals.
FAQ
1. What is the typical accuracy of a master meter prover?
A Coriolis master meter gives ±0.1% to ±0.15% of rate for mass and volume. An electromagnetic master offers ±0.2% of reading across a 100:1 turndown. Calibration certificates from accredited labs show typical expanded uncertainty of 0.05% to 0.1%.
2. Can you use a master meter prover for gas flow?
Yes, but the reference changes. For compressed air or natural gas, we select a thermal mass flow master or a Coriolis with high-pressure tube design. Gas provers require strict control of pressure and temperature at both meters, so we add a P-T compensation block on the skid.
3. What flow range can a portable prover cover?
With interchangeable master meters from DN10 to DN250, a mobile prover system covers flow ranges from 5 kg/h up to 500,000 kg/h of liquid. We often split large pipeline needs across two reference heads on the same skid.
4. Which reference meter works best for high-viscosity fluids?
Coriolis meters dominate here. Their tube geometry stays stable from water-like viscosity up to 600 cP, and they remain insensitive to velocity profile changes. A positive displacement master can also work for fuel oils above 1000 cP, but we rarely recommend it for portable rigs due to weight and cleanout issues.
5. How often should a master meter be recalibrated?
We recommend sending the reference meter to an ISO 17025 accredited lab every 12 months. If the master meter travels frequently between sites, an 8-month interval prevents borderline drift. Silver Instruments can handle the lab recalibration and return the master meter with a fresh certificate in under 10 working days.
Get a quote or technical sizing from Silver Automation Instruments. Send us your pressure (bar), temperature (°C), pipe size (DN), and flow range. Email [email protected], call +86-135-1213-1526, or message us on WhatsApp at 86-135-12131526. We custom-build the master meter prover so it lands ready to operate on your next maintenance shift.
 Hot Blog
 Related AD